There is a loss category in every solar PV feasibility study that looks small, gets approved without discussion, and then quietly erodes performance for 25 years.
It is not soiling. It is not thermal derating. It is not panel degradation.
It is the resistive loss in the DC cabling — the energy dissipated as heat in every meter of conductor between the solar panels and the inverter, governed by a physical law that does not care about monitoring systems, O&M protocols, or commissioning audits.
The formula is P = I²R. Power loss equals current squared multiplied by resistance. Two consequences follow directly from this formula that most feasibility studies underestimate:
First — resistive losses scale with the square of the current. Doubling the current quadruples the power loss. In a high-current industrial installation with string currents of 12 to 18 amperes on 580 Wp monocrystalline panels, the absolute power loss per meter of cable is significantly higher than in a residential system — and the economic case for upsizing cable cross-sections is correspondingly stronger.
Second — resistance increases with temperature. Copper resistance increases approximately 0.4% per degree Celsius. PV cables operating at 75°C exhibit roughly 25% higher resistance than room temperature values. A feasibility study that calculates DC resistive losses at 20°C standard — which describes every PVsyst simulation run with default settings — is systematically underestimating the losses that will actually occur during peak summer production hours in MENA and Africa.
These two consequences combine to create a performance gap that was present in the design, invisible in the monitoring data, and entirely preventable with a cable sizing methodology that reflects the actual operating conditions of the installation.
Disclosure: This article contains affiliate links. If you purchase through these links, I may earn a small commission at no extra cost to you. I only recommend technical resources that I consider genuinely useful for industrial solar professionals working in Africa and the MENA region.
What DC Resistive Losses Actually Are — And Where They Occur
DC voltage drop for solar cables is calculated using Vdrop = I × R × L, where I is the maximum circuit current, R is the cable resistance in ohms per meter, and L is the one-way cable length in meters. For a complete circuit, multiply by 2 to account for both positive and negative conductors.
In an industrial solar PV installation, resistive losses occur at five distinct points along the DC current path — each with its own loss magnitude and its own degradation trajectory over the project lifetime.
String DC cables — the primary loss location
The cables that connect panels within a string and carry string current to the combiner box account for the largest share of DC resistive losses on most C&I installations. Their loss depends on three variables: string current, cable cross-section, and total cable length per string.
On a ground-mounted industrial installation with strings of 20 panels arranged across a large footprint, string cable runs of 20 to 40 meters are common — significantly longer than rooftop applications where panels are concentrated in a compact area. At 15 A through a 2.5 mm² cable over 20 m, you lose roughly 3.5% of your power to resistive heating — and the cable runs hot enough to degrade its own insulation over time.
Main DC cables — the homerun loss
The cables connecting combiner boxes to inverters carry aggregated current from multiple strings — typically 4 to 8 strings per combiner box. Their current is proportionally higher, their cross-sections are larger, and their runs are often the longest DC cable segments on the installation. On combiner-to-inverter homeruns over 40 m, voltage drop almost always governs — the resistive loss over a long run requires a larger conductor than ampacity alone would mandate.
MC4 connectors and junction box terminals
Each MC4 connector pair has a nominal contact resistance below 0.5 milliohms when new. Over time — under the thermal cycling, UV exposure, and mechanical vibration of a MENA operating environment — this contact resistance increases. On a string with 20 panels and 40 MC4 connections, a contact resistance increase from 0.5 to 5 milliohms per connector represents an additional string resistance of 180 milliohms — generating measurable losses and localized heating detectable by thermal imaging.
Combiner box internal connections
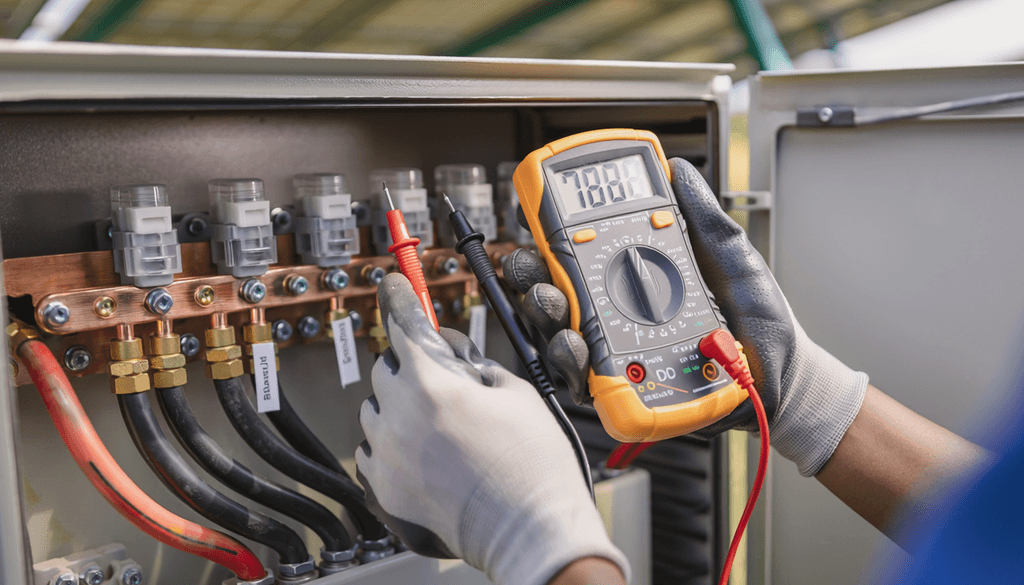
Fuse holders, bus bars, and terminal connections inside the combiner box contribute a small but non-negligible resistance to the DC circuit. Loose terminal connections — a common finding on installations that have undergone significant thermal cycling — can develop contact resistances that generate hot spots and production losses that monitoring systems attribute to string underperformance without identifying the root cause.
Inverter DC input terminals
The connection between the main DC cable and the inverter DC input terminal is the last resistance point in the DC circuit. Its contribution to total loss is small — but its degradation over time follows the same pattern as all DC connection points: progressive oxidation and mechanical loosening under thermal cycling.
The MENA Temperature Problem — Why Your Cable Loss Calculation Is Wrong
This is the field-specific insight that separates an accurate cable loss analysis from a standard simulation output.
The resistivity of copper at 20°C — the standard reference temperature used in PVsyst and most cable sizing tools — is 0.0172 Ω·mm²/m. The temperature coefficient of copper resistivity is approximately 0.39% per degree Celsius.
On an industrial installation in MENA where DC cables are routed in conduits or trays exposed to direct sunlight, peak cable temperatures during summer operation reach 60°C to 80°C — not 20°C. The resistivity at 70°C is approximately 0.0172 × (1 + 0.0039 × 50) = 0.0206 Ω·mm²/m — 20% higher than the standard reference value.
The practical consequence for a typical C&I industrial installation:
| Cable Condition | Resistivity | DC Resistive Loss | Annual Financial Impact per MWp |
|---|---|---|---|
| Standard calculation — 20°C | 0.0172 Ω·mm²/m | 0.8% to 1.2% of production | Reference baseline |
| Summer peak — MENA conduit 70°C | 0.0206 Ω·mm²/m | 1.0% to 1.5% of production | 3,600 to 5,400 USD additional |
| Aged connections — 5 years MENA | 0.0206 Ω·mm²/m + contact resistance | 1.3% to 2.0% of production | 9,000 to 14,400 USD additional |
The following curve shows what these three scenarios look like when their cumulative financial consequences are plotted across a 25-year project lifetime. The gap between the blue line and the red line — between what a standard 20°C calculation projects and what aged MENA connections actually deliver — is not visible in any single year’s monitoring data. It is only visible when the losses are accumulated across time. That is precisely why it is never discussed at the design stage and never corrected in operation.
Cumulative DC Resistive Loss Curve :
---
config:
  themeVariables:
    xyChart:
      plotColorPalette: "#3b82f6, #f97316, #ef4444"
---
xychart-beta
    title "Cumulative DC Resistive Losses per MWp - 3 Scenarios over 25 Years (USD)"
    x-axis [Y1, Y3, Y5, Y7, Y10, Y13, Y15, Y17, Y20, Y23, Y25]
    y-axis "Cumulative Loss USD per MWp" 0 --> 200000
    line [3600, 10800, 18000, 25200, 36000, 46800, 54000, 61200, 72000, 82800, 90000]
    line [5400, 16200, 27000, 37800, 54000, 70200, 81000, 91800, 108000, 124200, 135000]
    line [9000, 27000, 45000, 63000, 90000, 117000, 135000, 153000, 180000, 180000, 180000]
Legend: 🔵 Blue = Standard calculation 20°C — 90,000 USD at year 25 | 🟠 Orange = MENA reality 70°C — 135,000 USD | 🔴 Red = MENA aged connections 5 years — 180,000 USD
Over a 25-year project lifetime, the gap between the standard calculation and the MENA operational reality — combining temperature-corrected cable resistance and progressive contact resistance degradation — represents 90,000 to 180,000 USD per MWp in additional losses that were never included in the financial model.
The Three DC Cable Sizing Mistakes That Cost Money Over 25 Years
Mistake 1 — Using minimum regulatory cross-section rather than economic optimum
A cable can pass the ampacity check and fail the voltage-drop check, or pass voltage drop and fail ampacity. You run both, then select the larger resulting size. The constraint that governs depends on run length — on string runs under 20 m, ampacity almost always governs; on combiner-to-inverter homeruns over 40 m, voltage drop almost always governs.
The minimum cross-section required by IEC 62548 is calculated to prevent dangerous cable overheating — not to minimize energy losses over 25 years. These are different optimization objectives with different results.
On a string cable carrying 14 A over a 25-meter run, the minimum regulatory cross-section may be 4 mm². The economic optimum — calculated by comparing the incremental cost of upgrading to 6 mm² against the 25-year value of reduced resistive losses — is almost always 6 mm² on a MENA industrial installation where cable temperatures routinely exceed 60°C.
What to ask your EPC contractor: “Show me the economic cross-section optimization for each cable segment — comparing incremental material cost against 25-year present value of reduced losses at operating temperature.”
Good answer: A table showing both ampacity and voltage drop checks at temperature-corrected resistivity, with the economic comparison documented for each cable segment.
Red flag: “We sized to IEC 62548 minimum requirements.” Regulatory minimum and economic optimum are different calculations with different results — and in MENA conditions, they diverge significantly.
Mistake 2 — Not calculating cumulative voltage drop from panel to inverter
Industry best practice limits DC voltage drop to 1% to 2% for PV source circuits and 1% to 3% for DC output circuits. A 1% limit is recommended for systems where inverter efficiency is critical or where string voltage is already near the inverter’s minimum MPPT threshold.
The cumulative voltage drop from the farthest panel to the inverter — combining string cable drop, MC4 connector drop, combiner box terminal drop, and homerun cable drop — can exceed the recommended limit on large-footprint industrial installations if each segment is sized independently rather than as part of an integrated voltage drop budget.
When cumulative voltage drop exceeds the inverter’s MPPT operating range at low irradiance conditions, the inverter fails to track the maximum power point — generating production losses that no monitoring system will correctly identify as a cable sizing issue. They appear in the data as reduced yield at low irradiance — plausible, unalarming, and entirely attributable to normal operating conditions.
What to ask your EPC contractor: “Show me the cumulative voltage drop calculation from the farthest panel to the inverter under minimum irradiance conditions.”
Good answer: A complete voltage drop budget covering string cables, MC4 connectors, combiner box terminals, and homerun cables — with confirmation that cumulative drop stays within the inverter MPPT range at minimum operating irradiance.
Red flag: “String voltage drop is within 1% and homerun is sized separately.” Separate segment sizing misses the cumulative effect that determines inverter MPPT performance at low irradiance.
Mistake 3 — Ignoring contact resistance degradation in the economic analysis
Standard cable sizing analyses consider the initial resistance of new connections. They rarely include a provision for the progressive increase in contact resistance that occurs at every DC connection point under sustained thermal cycling in a MENA environment.
Field measurements on industrial installations confirm that MC4 connector contact resistance increases from below 0.5 milliohms at installation to 5 to 15 milliohms after 3 to 5 years in a demanding MENA operating environment. The financial consequence of this progressive degradation — affecting every one of the hundreds of MC4 connections on a typical C&I installation — is not included in any standard feasibility study loss model.
What to ask your EPC contractor: “What provision for contact resistance degradation is included in the 25-year energy yield model?”
Good answer: An explicit provision of 0.1% to 0.2% additional annual loss from year 3 onward, with the assumption documented and the MC4 connector inspection protocol specified in the O&M scope.
Red flag: “Connection losses are included in the standard cable loss model.” Standard cable loss models assume new connections with zero degradation — which describes no MENA installation after year three.
The DC Resistive Loss Cascade — From Panel to Inverter
The following diagram shows the complete path of DC resistive losses from panel output to inverter input — with the loss magnitude at each point under standard calculation conditions and under realistic MENA operating temperatures:
Flowchart DC:
flowchart LR
    A["Solar Panel<br>STC Output<br>100%"] --> B["String DC Cable<br>4mm² at 70°C<br>Loss 0.4% to 0.6%"]
    B --> C["MC4 Connectors<br>40 per string<br>Loss 0.15% to 0.4%"]
    C --> D["Combiner Box<br>Terminals and Fuses<br>Loss 0.05% to 0.15%"]
    D --> E["Main DC Homerun<br>6mm² to 16mm²<br>Loss 0.25% to 0.5%"]
    E --> F["Inverter DC Input<br>Terminals<br>Loss 0.05% to 0.1%"]
    F --> G["Inverter<br>DC Input<br>98% to 99%"]
    H["Standard calculation 20°C<br>Total loss 0.7% to 1.3%"] -.-> G
    I["MENA reality 70°C<br>Total loss 1.0% to 1.7%"] -.-> G
    J["MENA aged 5yr connections<br>Total loss 1.4% to 2.3%"] -.-> G

    style A fill:#ffd93d,color:#000
    style G fill:#51cf66,color:#fff
    style H fill:#74c0fc,color:#000
    style I fill:#fd7e14,color:#fff
    style J fill:#ff6b6b,color:#fff
Legend: 🟡 Yellow = panel output | 🟢 Green = inverter input | 🔵 Blue = standard 20°C | 🟠 Orange = MENA reality 70°C | 🔴 Red = MENA aged connections
What a Rigorous DC Cable Sizing Study Should Include for MENA Industrial Installations
Four elements that most DC cable sizing studies omit — and that determine whether the cable loss calculation reflects the installation that will actually be built and operated:
Element 1 — Temperature-corrected resistivity calculation
Every cable resistance calculation should use the resistivity at the expected maximum operating temperature of the cable — not the 20°C standard reference. For cables routed in conduits or trays exposed to direct sunlight in MENA, this means calculating resistance at 60°C to 80°C depending on installation configuration and local climate.
Element 2 — Economic cross-section optimization
For each cable segment, the sizing decision should be documented as an economic comparison: incremental material cost of the next larger cross-section versus 25-year present value of reduced resistive losses at the temperature-corrected resistance. On MENA industrial installations, this comparison almost always favors the larger cross-section by a significant margin.
The incremental material cost of upgrading from 4 mm² to 6 mm² across a typical C&I installation is approximately 8,000 to 15,000 USD per MWp. The 25-year value of reduced resistive losses from this upgrade is approximately 25,000 to 45,000 USD per MWp. The economic case for the upgrade requires no complex modeling — it requires only that the comparison be made at the design stage, before the cable specification is fixed.
Element 3 — Cumulative voltage drop budget from panel to inverter
The voltage drop calculation should cover the complete DC current path — from the farthest panel through string cables, MC4 connectors, combiner box terminals, homerun cables, and inverter input terminals — and confirm that the cumulative drop remains within the inverter’s MPPT operating range under minimum irradiance operating conditions.
Element 4 — Contact resistance degradation provision
The energy loss model should include a provision for progressive contact resistance increase at MC4 connectors and terminal connections — calibrated to the thermal cycling environment of the specific installation location. A conservative provision of 0.1% to 0.2% additional annual loss from year 3 onward produces a more accurate 25-year energy yield model than the zero-degradation assumption most feasibility studies apply.
For engineers and project developers who want to build the quantitative framework needed to perform rigorous DC cable sizing for industrial solar installations — Photovoltaic Systems Engineering by Messenger and Abtahi provides one of the most analytically complete treatments available of DC system design and its interaction with energy yield, inverter performance, and long-term financial outcomes.
The Inspection Protocol for DC Connections — Integrated Into the Monthly Field Cycle
The DC connection inspection activities below integrate directly into the monthly field protocol established in earlier analysis on this platform — specifically into Week 3 of the inspection cycle, which covers thermal and electrical inspection. The quarterly thermal imaging of DC connections warrants higher inspection frequency than panel-level degradation in MENA thermal cycling environments.
Quarterly thermal imaging of DC connections
During Week 3 of the monthly inspection cycle, extend the thermal imaging scope to include combiner box terminals, homerun cable terminations at the inverter, and a sample of accessible MC4 connectors under operating load. Any connection showing a temperature differential of more than 10°C above ambient warrants immediate follow-up.
Annual MC4 pull-test program
A systematic pull-test of all accessible MC4 connectors — confirming that retention force meets the manufacturer’s specification — identifies connections that have lost their mechanical integrity before they develop significant resistance increases. The cost is labor and time. The consequence of not performing it is undetected resistance increase at hundreds of connection points across the array.
Biannual DC resistance measurement
Using a calibrated milliohm meter on a sample of accessible string terminations, measure DC resistance from panel terminal to combiner box terminal and compare against the commissioning baseline. A resistance increase of more than 20% above the commissioning measurement identifies a degrading connection pathway that thermal imaging may not yet have detected.
DC resistive losses are the performance gap that was designed in — calculated with an assumption that underestimates the actual operating temperature of the cables, approved without economic optimization of the cross-section, and left to compound across 25 years without a monitoring system that can detect their progressive deterioration.
Cable losses are permanent. You cannot fix them with monitoring or maintenance after the fact. Size correctly once, and the system performs for 25 years. Size to the regulatory minimum without economic optimization in a MENA climate, and the gap compounds silently from day one.
The return on investment of correct DC cable sizing at the design stage is among the highest available in industrial solar engineering: an additional investment of 8,000 to 15,000 USD per MWp in cable material generates a 25-year return of 90,000 to 180,000 USD per MWp in avoided losses — a ratio of 6:1 to 12:1 on the incremental investment. No O&M intervention, no monitoring upgrade, and no panel technology choice available at the design stage offers a comparable return on an investment of this magnitude. The only requirement is that the economic comparison is made before the cable specification is finalized — not after the cables are pulled.
The gap between a DC cable system designed at 20°C standard conditions and one designed for the actual thermal environment of a MENA industrial installation — combined with the progressive contact resistance degradation that thermal cycling produces over 5 to 10 years — represents a cumulative performance difference of 90,000 to 180,000 USD per MWp over a 25-year project lifetime.
This gap does not appear in any monitoring report. It does not generate any alarm. It is simply the difference between what the installation was designed to produce and what it actually produces — embedded in the cable sizing specification, confirmed at every peak summer operating hour, and compounding silently across decades.
The correction costs 8,000 to 15,000 USD per MWp in additional cable material at the design stage.
The omission costs six to twelve times that amount over the project lifetime.
That calculation does not require a spreadsheet. It requires only that someone makes it before the cable specification is finalized.
The DC connection thermal imaging findings, cable temperature observations, and MC4 connector resistance context referenced in this article reflect direct field measurement on an industrial solar installation in MENA — where peak summer cable temperatures, combiner box terminal conditions, and the progressive resistance increase at MC4 connectors after two years of operation are documented with calibrated instruments.
For engineers building or reviewing the DC design of a MENA industrial installation — the MENA Industrial Solar Data Guide provides the operational reference point that makes the temperature-correction argument concrete: what peak summer DC currents look like on a real installation, and what the cable system is actually asked to carry during those hours.
Get the Free Preview
The first 8 pages of the MENA Industrial Solar Data Guide — real Performance Ratio data, soiling measurements, and thermal derating figures from an industrial installation— No spam, just real data.
Disclosure: This article contains affiliate links. If you purchase through these links, I may earn a small commission at no extra cost to you. I only recommend technical resources that I consider genuinely useful for industrial solar professionals working in Africa and the MENA region.
Publié par :
Solar PV MENA Expert